© 2025 Messer Cutting Systems, Inc.
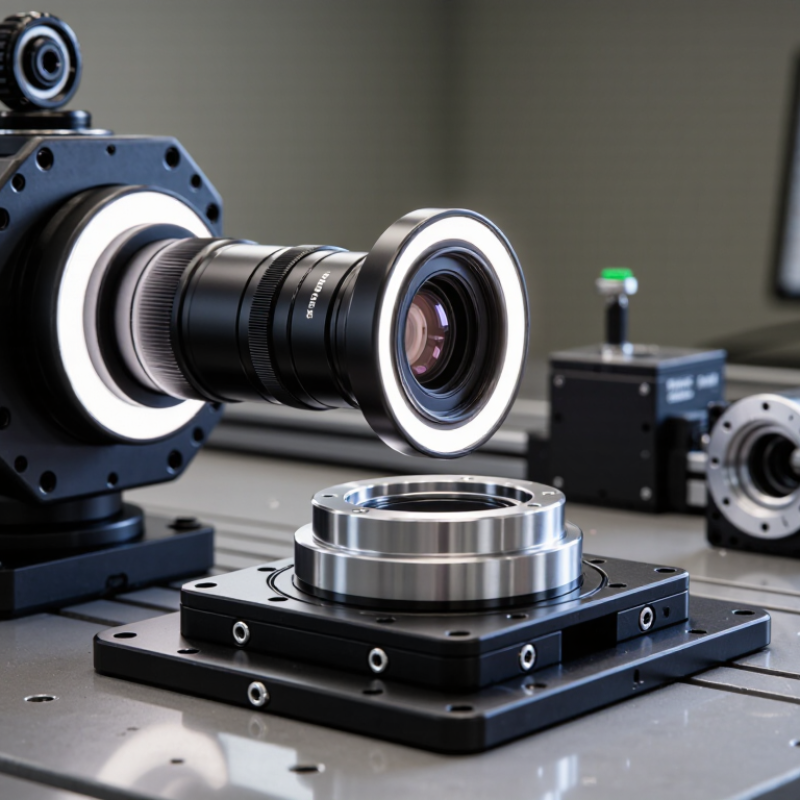
Choosing the best telecentric lens c mount is not a simple matter of matching threads. The mount must support the lens mechanically, optically, and operationally. A small mismatch can create image tilt, unstable focus, or unwanted measurement error.
Dr. John E. Greivenkamp, an optical design educator, has stated, “Optical design is always a compromise.” That principle applies directly here. A C-mount camera may offer convenient installation, yet its sensor size, flange focal distance, and pixel resolution must suit the lens. Check the 1-inch-32 thread carefully. Then inspect the camera’s mounting shoulder and available adjustment range. Do not assume every C-mount camera reaches the correct image plane.
The working distance deserves equal attention. Imagine a metal part positioned 100 millimeters below the lens, with a bright ring light reflecting from its edge. A telecentric design can preserve dimensional consistency, but only within its specified object-space range. Outside that range, perspective errors may return. They can be subtle. Sometimes, painfully subtle.
This guide examines magnification, sensor coverage, working distance, illumination, thread quality, and system alignment. It also considers practical issues, including vibration, thermal drift, and calibration. A perfect lens on a poorly aligned camera still produces unreliable measurements. That is easy to overlook. I have seen specifications look correct while the final image remained disappointing. Careful testing with the actual part is therefore essential. The best telecentric lens c mount is not necessarily the most expensive option. It is the one that fits the complete inspection system, including its limitations.
How to Choose the Best China Telecentric Lens C Mount?
What Is a C-Mount Telecentric Lens?
A C-mount telecentric lens is an industrial imaging lens with a standardized threaded interface. It connects to compatible cameras through a 1-inch, 32-thread mount. Its telecentric optical design keeps image size nearly constant when object distance changes slightly. This reduces perspective errors during measurement.
In practical inspection work, this matters when checking edges, holes, pins, or molded parts. A normal lens may make a near edge appear larger than a far edge. A telecentric lens keeps both edges more consistent. Object-space telecentric models are common for dimensional inspection. Bi-telecentric designs can improve accuracy further, but they usually cost more and need careful alignment.
Tips: Match the lens magnification to the sensor and feature size. Check the working distance before installation. Confirm the C-mount thread, sensor coverage, distortion data, and lighting clearance. A lens that fits mechanically may still produce dark corners or incomplete images.
Do not choose by magnification alone. Resolution, depth of field, aperture, and field of view must work together. In my experience, a slightly wider field can simplify positioning, but it may reduce measurement detail. Check the manufacturer’s test data, then verify performance with your actual camera and sample parts. Even a reliable specification can behave differently under uneven lighting, vibration, or imperfect alignment.
| Selection Dimension | Typical Specification or Range | Why It Matters | Recommended Selection Guidance |
|---|---|---|---|
| Mount Standard | C-mount, 1 inch–32 UN-2A thread; nominal flange focal distance of 17.526 mm | Determines mechanical compatibility between the lens and camera. | Confirm that the camera uses a C-mount rather than a CS-mount. Check thread engagement and available clearance. |
| Telecentric Design | Object-space, image-space, or bi-telecentric configuration | Telecentric optics reduce perspective error and keep measured dimensions more consistent when object height changes. | Choose object-space telecentricity for dimensional inspection. Choose bi-telecentric optics when both object and image-side accuracy are critical. |
| Magnification | Common fixed values include approximately 0.1× to 1.0×; higher values are available for smaller fields of view | Magnification determines the relationship between object size and its image on the sensor. | Select magnification using: magnification = sensor dimension ÷ required object field dimension. |
| Sensor Format | Typically compatible with 1/3-inch, 1/2-inch, 2/3-inch, 1-inch, or larger sensors, depending on the image circle | An image circle that is too small causes corner shading or vignetting. | Choose a lens image circle equal to or larger than the camera sensor format, and verify the actual sensor diagonal. |
| Working Distance | Common working distances are approximately 40–200 mm, depending on optical design | Working distance affects lighting space, object access, safety, and system installation. | Allow enough clearance for illumination, fixtures, moving parts, and protective windows. |
| Field of View | Determined by sensor size and magnification; lower magnification provides a larger field of view | The field of view must contain the complete part, including positioning tolerance. | Add practical margin around the target area rather than matching the part size exactly. |
| Telecentricity Error | Often specified in milliradians; lower values indicate better control of perspective effects | A lower angular error improves dimensional repeatability across object-height variations. | For precision measurement, request the measured telecentricity specification rather than relying only on the term “telecentric.” |
| Distortion | Low-distortion designs may specify less than 0.1%; the actual value depends on magnification and optical structure | Distortion changes the apparent position of features across the image and can affect measurement accuracy. | Use the calibrated distortion value for metrology applications and verify it over the complete field of view. |
| Resolution | Specified in line pairs per millimetre or by the smallest resolvable feature | Resolution determines whether edges, holes, scratches, and other features can be separated clearly. | Match optical resolution to pixel size, lighting quality, and the smallest feature that must be inspected. |
| Aperture and Depth of Field | Many telecentric lenses use a fixed or adjustable aperture; depth of field increases as the aperture is stopped down | A larger depth of field helps maintain focus across uneven or vertically varying parts. | Balance depth of field against light throughput and diffraction. Stopping down too far can reduce resolution. |
| Spectral Range | Visible-light models commonly cover approximately 400–700 nm; some models support near-infrared wavelengths | Optical performance, focus, and transmission can change with wavelength. | Specify the illumination wavelength and confirm transmission and chromatic performance before purchase. |
| Coating and Lighting Compatibility | Anti-reflection coatings designed for visible or selected spectral bands; coaxial, backlight, or ring-light setups may be used | Proper coating and illumination improve contrast, reduce flare, and reveal the required features. | Select the lens and lighting system together, especially for reflective, transparent, or low-contrast parts. |
| Mechanical Adjustment | Some models provide focus adjustment, iris adjustment, locking rings, or mounting interfaces | Adjustment features simplify alignment and help maintain a stable inspection setup. | Prefer locking adjustments for vibration-prone production lines and verify the available mounting space. |
| Best-Fit Application | Dimensional measurement, gauging, alignment, semiconductor inspection, electronics inspection, and machine vision | Telecentric lenses are most valuable when measurement repeatability and low perspective error are priorities. | For general inspection without strict dimensional requirements, a conventional machine-vision lens may be more economical. |
Note: Specifications are representative industry ranges. Confirm the exact optical, mechanical, and environmental specifications for the intended camera, sensor, illumination, and measurement tolerance.