© 2025 Messer Cutting Systems, Inc.
Buying a Roller Conveyor for international operations is not simply a matter of comparing prices. The right choice must fit your products, facility, workforce, and future production plans. A small carton, a steel frame, and a pallet each create different demands on rollers, bearings, and conveyor structure.
Dr. M. G. Kay, a recognized material-handling specialist, states, “Equipment selection should be based on the complete material-handling system, not on one component alone.” That principle remains highly practical. Buyers should examine load weight, carton dimensions, roller diameter, pitch, frame width, speed, and accumulation requirements. A useful test is simple: place the heaviest expected load on a sample section and watch for deflection, noise, or unstable movement.
Think beyond the showroom.
Global purchasing also requires careful attention to motor voltage, control compatibility, packaging, spare parts, installation guidance, and after-sales support. A low quotation may become expensive when replacement bearings take weeks to arrive. Ask for drawings, load calculations, warranty terms, and documented factory testing. Verify whether the supplier has experience with your product type and operating environment.
Some decisions will remain imperfect. Forecasts change. Space becomes limited. A conveyor selected for today may restrict tomorrow’s layout. That is why these ten buying tips focus on practical evidence, transparent communication, and total ownership cost. The goal is not the most sophisticated Roller Conveyor. It is a reliable system that moves goods safely, consistently, and efficiently across real working conditions.
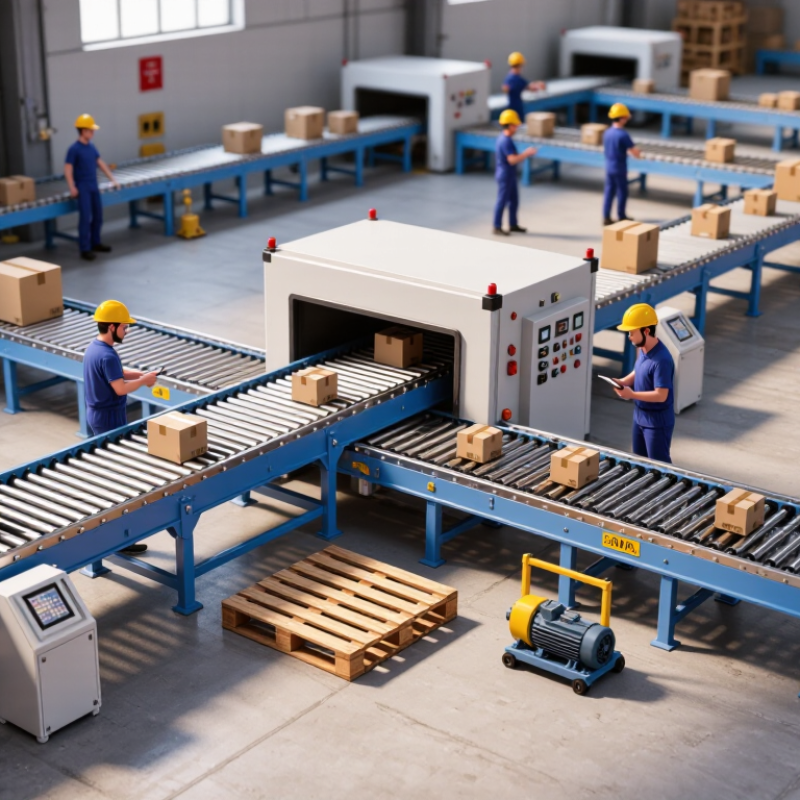
Choosing a roller conveyor starts with the product, not the catalog. Straight gravity conveyors suit cartons, totes, and short-distance transfers. Powered roller conveyors handle heavier loads and controlled accumulation. Flexible conveyors help temporary packing areas, but their uneven expansion can affect alignment. I have seen buyers specify “heavy duty” without stating pallet weight, base condition, or daily cycles. That shortcut creates costly redesigns.
Application data should guide every purchase. The U.S. Census Bureau reported that e-commerce represented 16.1% of total U.S. retail sales in 2024. That volume increases pressure on picking, sorting, and dispatch lines. Measure peak cartons per minute, load dimensions, weight range, and required accumulation distance. Then check roller diameter, pitch, frame strength, motor torque, and belt or chain configuration. Small cartons may need closer roller spacing to prevent tipping. Dusty facilities may require sealed bearings and simpler guarding.
MHI’s 2024 Annual Industry Report found that 55% of supply-chain leaders planned to increase technology investment within two years. Automation, however, is not always the correct answer. A powered line can waste energy when operators load irregularly. Review noise limits, cleaning routines, maintenance access, and emergency-stop locations with actual users. CEMA guidance can support dimensional and safety decisions, but local requirements still need verification. Do not trust a single test carton. Run mixed loads at peak speed, because the weakest package often reveals the real design problem.
| No. | Buying Tip | Suitable Conveyor Type | Key Application Requirement | Typical Selection Guidance | Important Specification | Buyer Verification Checklist |
|---|---|---|---|---|---|---|
| 1 | Define the load first | Gravity, powered, or chain-driven roller conveyor | The conveyor must carry the heaviest individual unit and the total accumulation load without excessive deflection. | Select a rated capacity above the maximum operating load, not only the average load. Include pallet, carton, container, or tote weight. | Common light- to medium-duty systems handle approximately 50–250 kg per unit; heavier systems require reinforced frames and rollers. | Confirm unit weight, load distribution, base condition, impact during loading, and the required safety factor with the supplier. |
| 2 | Match the roller diameter to the load | Gravity or powered roller conveyor | Rollers must provide adequate contact area and resist bending under the working load. | Small cartons may use smaller rollers, while pallets and heavy containers normally require larger-diameter rollers and stronger shafts. | Typical roller diameters include about 38, 50, 60, 76, and 89 mm, depending on load and frame design. | Check roller material, wall thickness, shaft diameter, bearing type, roller load rating, and deflection under full load. |
| 3 | Choose the correct roller pitch | Gravity, powered, and accumulation roller conveyor | The product should rest on enough rollers at all times to remain stable and move smoothly. | A common design rule is to maintain at least three rollers under the shortest rigid load during transport. | Typical center-to-center pitches range from approximately 50–150 mm; heavier or irregular loads usually need closer spacing. | Provide the shortest package length, package base dimensions, product rigidity, and required transfer orientation. |
| 4 | Select gravity or powered operation | Gravity roller versus motor-driven roller conveyor | Gravity systems need manual pushing or a controlled slope; powered systems provide consistent movement and automation. | Use gravity for simple, low-throughput movement. Use powered rollers for long lines, high throughput, controlled speed, or accumulation. | Powered conveying commonly operates around 0.1–0.5 m/s, but the required speed depends on product stability and process timing. | Confirm throughput per hour, conveyor length, elevation change, start-stop frequency, noise limits, and available power supply. |
| 5 | Check conveyor width and product fit | All roller conveyor types | The conveyed unit must remain supported and guided without rubbing the frame or falling between side rails. | For straight conveying, the usable roller width is commonly selected slightly wider than the product base width. | Typical conveyor widths range from approximately 300–1,200 mm, with custom widths available for oversized loads. | Measure maximum and minimum product width, base shape, side-clearance needs, guide-rail position, and transfer points. |
| 6 | Consider curves and transfers | Tapered-roller curve or multidirectional transfer section | Curves require stable product tracking, while transfers must bridge gaps without catching package edges. | Use tapered rollers for curved paths and ball-transfer or pop-up units when products must change direction or conveyor line. | Curve radius, roller taper, transfer gap, and product center of gravity affect tracking and safe operation. | Submit a layout drawing, product dimensions, turning direction, minimum turning radius, and transfer-height tolerances. |
| 7 | Specify the operating environment | Painted steel, galvanized steel, or stainless-steel conveyor | Moisture, dust, chemicals, temperature, and washdown conditions determine the suitable materials and protection level. | Use corrosion-resistant construction in humid or wet areas and sealed components where dust or liquid ingress is expected. | Stainless steel is commonly preferred for frequent washdown or hygienic environments; surface treatment depends on exposure. | State ambient temperature, humidity, washdown method, chemical exposure, dust level, indoor/outdoor location, and cleanliness requirements. |
| 8 | Plan accumulation and product control | Zero-pressure accumulation or zoned powered roller conveyor | Products may need to queue without collision, back pressure, package damage, or uncontrolled release. | Use individually controlled zones with sensors for fragile goods, automated lines, and variable production flow. | Zone length is often based on the longest load plus clearance; sensor logic and release spacing must match throughput. | Confirm product fragility, accumulation quantity, release sequence, sensor type, control interface, and emergency-stop arrangement. |
| 9 | Verify motor, drive, and electrical standards | Belt-driven, chain-driven, or motorized roller conveyor | The drive system must provide sufficient starting torque and match the destination country's electrical requirements. | Variable-speed drives are useful where line speed changes, while fixed-speed drives suit simple material-flow applications. | Common industrial supplies include 230 V or 400 V three-phase power at 50 or 60 Hz, depending on the market. | Confirm voltage, frequency, phase, motor protection, control voltage, plug and wiring requirements, documentation, and local compliance. |
| 10 | Evaluate safety, maintenance, and total cost | Any conveyor type, configured for the site's risk level | The system should be safe to operate, easy to inspect, and economical throughout its service life. | Include guarding, emergency stops, pinch-point protection, access clearance, spare parts, installation, and training in the purchase decision. | Maintenance access should allow inspection of bearings, rollers, chains, belts, sensors, and drive components without unsafe exposure. | Request manuals, risk assessment information, spare-parts lists, warranty terms, service response details, and installation requirements. |
Note: The dimensional and performance ranges shown are typical planning references. Final conveyor selection should be validated through a detailed load, layout, environment, safety, and throughput assessment.